Specifying a Sintered 316L powder filter cartridge in refinery and petrochemical assets is a metallurgical and process decision, not a catalog pick. Formed by cold-pressing 316L/304L stainless steel powder and solid-state sintering at 1,100–1,300°C, the cartridge yields a monolithic, porous tube with 30–50% engineered porosity and absolute ratings from 0.5–70 µm. Its tortuous, 3D-interconnected pore network enables depth filtration—capturing solids throughout the wall rather than on a surface skin—with no binders to delaminate or shed. This construction is especially useful when the process requires stable filtration under pressure, temperature cycling, solvent exposure, and repeated cleaning. The correct specification must therefore connect alloy selection, particle-size distribution, flow conditions, cleaning method, and documentation requirements rather than focusing on micron rating alone. Every sintered metal powder filter is specified against the actual process conditions, never against a catalogue number alone.
Sintered 316L Powder Filter Cartridge in FCC Slurry Service
The primary application is catalyst recovery: in FCC and hydrotreating, zeolite/alumina fines escape reactors; the cartridge retains them (outside-in) for backwash as concentrated slurry, returning value instead of landfill waste. In practical terms, the filter must maintain capture efficiency while handling fluctuating solids loading, viscosity, and differential pressure. A robust design also needs enough open area to avoid rapid blinding during startup or upset conditions.
For precious-metal hydrogenation (Pd/C, Pt/C), 0.5–5 µm ratings recover >99% catalyst when the element is correctly sized and operated within its design flux. FCC slurry-oil filtration handles 1,000–3,000 ppm fines in high-viscosity hydrocarbon at ~350°C continuous, with backflush excursions to 650°C. Other duties include polymer melt gel removal, amine and glycol polishing, lube-oil clarification, jet-fuel protection, and the removal of corrosion products before sensitive downstream equipment. Before finalizing the element, confirm the actual contaminant size distribution, solids concentration, flow rate, viscosity, operating temperature, and allowable clean and terminal ΔP.
Comparison: Powder-Sintered vs. Wire Mesh vs. Polymer
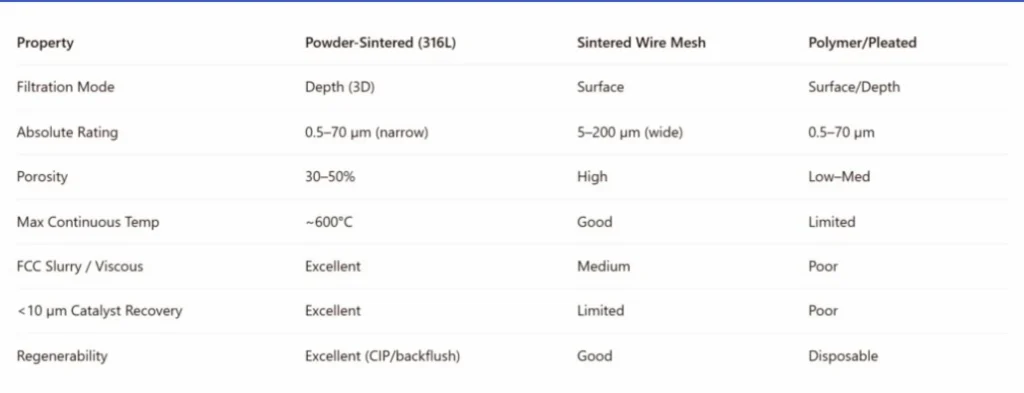
Powder-sintered elements provide a rigid, depth-filtration structure with strong resistance to heat and many aggressive process fluids. Compared with polymer pleated media, they are better suited to high-temperature service and repeated regeneration, although their initial cost may be higher. Wire mesh offers a defined surface opening, easy visual inspection, and low resistance in many applications, but it may be less effective when fine particles must be captured through the depth of the media. Polymer cartridges can be economical for lower-temperature, disposable service, but compatibility, swelling, oxidation, and thermal limits must be checked carefully. The best choice is the one that meets separation performance and total operating cost, including cleaning, replacement, catalyst recovery, and disposal. For a broader comparison of powder filter media, materials, shapes, and pore structures, see this sintered powder filter element comparison guide.
Selection Logic
Alloy: 316L default for chloride/acid; sour gas (H₂S/CO₂) demands lab-corrosion data—upgrade to Hastelloy/Inconel/Monel if marginal. Housing: HIC-resistant carbon steel (NACE MR0103) or 316L. Micron rule: FCC fines 5–20 µm; precious-metal 0.5–5 µm; polymer melt 10–25 µm. Over-specifying raises ΔP and blinding; under-specifying contaminates downstream.
Also define the flow direction, sealing arrangement, connection standard, element dimensions, and support configuration. Ask for a bubble-point or integrity-test requirement if filter failure could affect product quality or safety. For sour or corrosive service, review chloride level, water content, hydrogen exposure, temperature, and cleaning chemistry together; no single material grade guarantees suitability for every process stream. A pilot test or sample evaluation is valuable when the feed contains deformable solids, catalyst fines with a broad PSD, or material that may compress inside the pores.
Regenerability & Economics
CIP (alkali soak → high-pressure rinse → acid wash → bubble-point verification per EN 10204 3.1/3.2) restores >90% permeability. Life extends to years; high-temp bake must avoid prolonged carburizing embrittlement. Cleaning should be based on the actual foulant: oil, polymer, catalyst, scale, and metal sulfide deposits may require different chemistry and sequence. Record initial permeability, clean pressure drop, operating pressure drop, cleaning cycles, and final integrity results so the maintenance team can identify gradual damage or irreversible blinding.
Total cost of ownership should include recovered catalyst value, reduced waste, labor, cleaning chemicals, spare elements, downtime, and protection of downstream pumps or membranes. A cartridge with a slightly higher purchase price can be more economical if it survives more cycles and produces a consistent, verifiable filtrate. Conversely, selecting an unnecessarily tight rating can increase energy consumption and shorten service life, so the design should balance separation performance against flux and cleanability.
Frequently Asked Questions
1. How to select the correct micron rating for FCC slurry and catalyst recovery service?
Start with the actual contaminant particle-size distribution, not only the nominal target size. FCC fines commonly require a 5–20 µm range, while precious-metal catalyst recovery may require approximately 0.5–5 µm. The selected rating must balance capture efficiency, solids loading, viscosity, clean pressure drop, terminal differential pressure, and the risk of rapid blinding.
2. How to verify whether a sintered 316L powder cartridge is suitable for sour or corrosive petrochemical service?
Evaluate chloride concentration, water content, hydrogen exposure, H₂S/CO₂ levels, temperature, pressure, and cleaning chemistry together. 316L may be suitable for many streams, but alloy selection should be supported by corrosion data and process-specific validation; severe or marginal conditions may require a nickel alloy or another upgraded material. Housing material and NACE requirements should also be reviewed.
3. How to design a cleaning and regeneration program without damaging the filter cartridge?
Match the cleaning sequence to the foulant: oil, polymer, catalyst fines, scale, and metal sulfides may require different chemical and thermal treatments. Define alkaline soaking, rinsing, acid washing, backflushing, or baking conditions according to the cartridge material and process limits. Record clean permeability, operating pressure drop, cleaning cycles, and post-cleaning integrity results to identify irreversible blinding or structural damage.
4. How to prove that a sintered powder cartridge meets petrochemical quality and integrity requirements?
Specify the required material certificate, dimensional inspection, permeability data, filtration rating, weld inspection, and bubble-point or other integrity test before production. For controlled procurement, request EN 10204 3.1 or 3.2 documentation where applicable and ensure the test results correspond to the actual production batch. A pilot trial is advisable when the feed contains compressible solids, broad particle-size distributions, or high-value catalyst.
Engineering Support for Your Petrochemical Filtration Specification
Submit your stream data—flow, T, contaminant PSD, recovery aim—and receive matched alloy, rating, and TCO comparison. Include the process phase, pressure, viscosity, cleaning temperature, expected cycle length, housing information, and any required inspection or material certificates. With these inputs, the specification can address filtration efficiency, mechanical strength, corrosion margin, regeneration, documentation, and long-term operating cost before the equipment is released for purchase.